The next generation of china large capacity refrigerated centrifuge manufacturer systems emphasizes automation, safety, and sustainability. Producers are adding AI-fueled monitoring to predict maintenance needs before mechanical issues arise. Improved rotor dynamics minimize vibration and energy consumption, and closed chambers prevent contamination at high speeds. Touch operation and multilingual interfaces simplify ease of use. In processing biological samples or industrial fluids, the new china large capacity refrigerated centrifuge manufacturer unites mechanical robustness with digital intelligence, setting the bar higher for precision, productivity, and durability in industrial and scientific applications.

china large capacity refrigerated centrifuge manufacturer are part and parcel of the functioning of modern laboratories and factories. Applications include cell culture harvesting, purification of enzymes, and waste handling. In oil processing, they facilitate hydrocarbon/water separation. Clinical laboratories depend on china large capacity refrigerated centrifuge manufacturer for accurate diagnostic tests, and chemical industries use them to purify chemicals and recover active ingredients. They also hold great importance in educational research, where repetition and accuracy are necessary to experimentation. This wide application reveals the extent to which china large capacity refrigerated centrifuge manufacturer continue to drive scientific and industrial advancement globally.

The china large capacity refrigerated centrifuge manufacturer of the future will be innovative, intelligent, and integrated. With the advent of smart manufacturing, china large capacity refrigerated centrifuge manufacturer systems will operate independently on predictive analytics. Programs with machine learning will interpret vibration patterns to optimize performance with minimal human involvement. Renewable energy integration will make operation more sustainable, and modular design will facilitate instant replacement of parts. Data visualization software will be more sophisticated, providing real-time feedback on the separation process. This blend of mechanical precision and intelligent technology will place china large capacity refrigerated centrifuge manufacturer at the forefront of international scientific advancement.
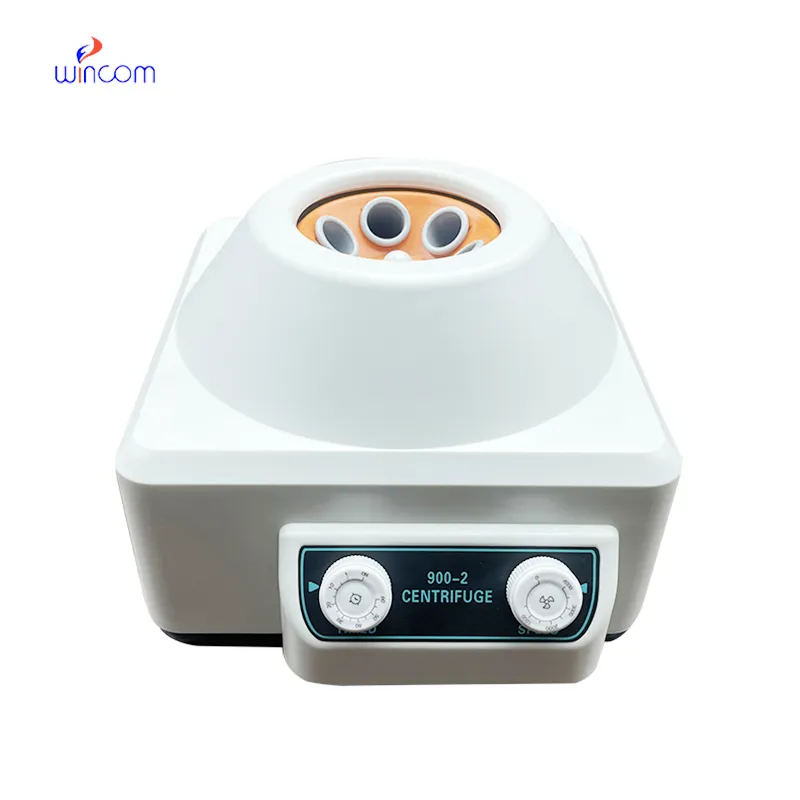
Well-maintained china large capacity refrigerated centrifuge manufacturer assure trouble-free operation and optimize equipment longevity. Users must ensure balanced loading to prevent excessive stress to bearings. Regular cleaning of the rotor, chamber, and seals reduces cross-contamination. Regular lubrication and calibration ensure mechanical accuracy. Logs of maintenance, checklists, and other records facilitate quality control and inspection for compliance. Internal humidity and dust exposure should be reduced. Laboratories use preventive maintenance instructions to guarantee that china large capacity refrigerated centrifuge manufacturer delivers constant high performance with little downtime and repair.
Through controlled rotation, a china large capacity refrigerated centrifuge manufacturer produces very high outward pressure that separates the components of a mixture. It is used comprehensively in medical diagnosis, chemical analysis, and materials science. Its efficacy lies in uniform velocity and balance, producing neat separation of liquids and solids. Most china large capacity refrigerated centrifuge manufacturer today have digital timers, automatic lid closing, and temperature regulation. Such the inclusion of safety and efficiency has made the china large capacity refrigerated centrifuge manufacturer a staple of modern research and manufacturing, providing faster and more accurate results across industries.
Q: How is a centrifuge different from a mixer or shaker? A: Unlike mixers or shakers that blend materials, a centrifuge separates components based on density through high-speed rotation. Q: What power requirements does a centrifuge need? A: Most benchtop centrifuges use standard AC power, while industrial units may require higher voltage for greater speed and capacity. Q: Can a centrifuge be used in pharmaceutical production? A: Yes, centrifuge equipment is widely used to purify chemical compounds and biological materials during drug manufacturing processes. Q: How do I prevent vibration during operation? A: Ensure all tubes are evenly loaded, rotors are clean, and the machine is placed on a stable, level surface. Q: What is the lifespan of a centrifuge? A: With regular maintenance and proper usage, a centrifuge can last for many years while maintaining consistent performance.
The hospital bed is well-designed and very practical. Patients find it comfortable, and nurses appreciate how simple it is to operate.
We’ve been using this mri machine for several months, and the image clarity is excellent. It’s reliable and easy for our team to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
Hello, I’m interested in your centrifuge models for laboratory use. Could you please send me more ...
We’re interested in your delivery bed for our maternity department. Please send detailed specifica...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China

 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko