In modern-day lab environments, the large capacity refrigerated centrifuge manufacturer is not just a separation apparatus—it is precision engineering. With simple-to-view digital displays and microprocessor controls, it makes it easy for scientists to quickly adjust variables like acceleration and deceleration rates. Other models come equipped with onboard diagnostics that analyze rotor condition and operating performance. High-end safety features like automatic lid interlocks and imbalance detection offer protection at every cycle. With more rapid and consistent processing needed in industries, large capacity refrigerated centrifuge manufacturer technology keeps up with stability, precision, and greater throughput capability.

From research in the laboratory to large-scale production, large capacity refrigerated centrifuge manufacturer devices have a place in processes requiring precision and efficiency. They purify reaction mixtures and solvents in chemical production. Hospitals rely on large capacity refrigerated centrifuge manufacturer for the testing of patients and therapeutic treatment. In farming, large capacity refrigerated centrifuge manufacturer are used to study plant biology and develop fertilizer formulations. In brewing and winery operations, they provide consistency within products by filtering out impurities. Even environmental engineers rely on large capacity refrigerated centrifuge manufacturer to filter sediment as well as identify contaminants. Such wide-ranging functionality demonstrates its vital position in contemporary technology and applied sciences.

large capacity refrigerated centrifuge manufacturer will integrate digital intelligence and cutting-edge engineering in the years to come. Complex algorithms will auto-tune parameters for optimum efficiency and safety. Energy-optimized designs will keep operating costs at a minimum and help support global green efforts. Robotics integration will facilitate round-the-clock unattended operation in big production setups. Modular design will provide ease of customization, allowing users to set up large capacity refrigerated centrifuge manufacturer for specific scientific or industrial uses. These improvements will allow large capacity refrigerated centrifuge manufacturer to not only increase performance but also establish new standards for automation, accuracy, and sustainability in the lab environments of the future.
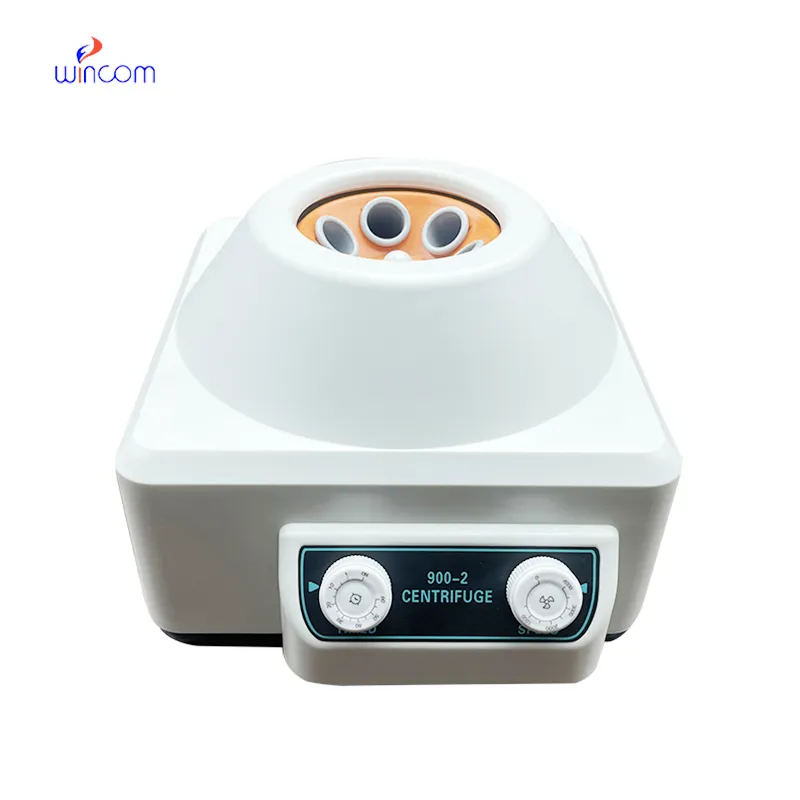
Proper care routines prolong the life of large capacity refrigerated centrifuge manufacturer significantly. Operators should inspect the rotor for corrosion or scratches after each use and clean with non-abrasive substances. The lid and chamber should be free from residue to prevent contaminations. Frequent lubrication of mechanical interfaces ensures effortless movement. Temperature and humidity control in the storage room protect internal parts against damage. A maintenance record helps track service time and early wear detection. Ongoing maintenance of these factors allows large capacity refrigerated centrifuge manufacturer to perform reliably for decades.
large capacity refrigerated centrifuge manufacturer is a piece of mechanical equipment that separates simple mixtures into differentiated parts by utilizing quick spinning. It functions by employing centrifugal force, which expels heavier elements and brings lighter elements closer towards the axis. This principle makes crucial work possible in microbiology, pharmaceuticals, and materials science. High-speed models can achieve exceptional separation accuracy in mere minutes. Modern large capacity refrigerated centrifuge manufacturer feature digital interfaces, temperature control, and advanced safety locks to ensure operation. They are so fast and versatile that they are a must-have asset for any laboratory or manufacturing plant.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
The water bath performs consistently and maintains a stable temperature even during long experiments. It’s reliable and easy to operate.
We’ve been using this mri machine for several months, and the image clarity is excellent. It’s reliable and easy for our team to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re interested in your delivery bed for our maternity department. Please send detailed specifica...
We’re looking for a reliable centrifuge for clinical testing. Can you share the technical specific...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China

 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko