In modern-day lab environments, the large capacity refrigerated centrifuge supplier is not just a separation apparatus—it is precision engineering. With simple-to-view digital displays and microprocessor controls, it makes it easy for scientists to quickly adjust variables like acceleration and deceleration rates. Other models come equipped with onboard diagnostics that analyze rotor condition and operating performance. High-end safety features like automatic lid interlocks and imbalance detection offer protection at every cycle. With more rapid and consistent processing needed in industries, large capacity refrigerated centrifuge supplier technology keeps up with stability, precision, and greater throughput capability.

The utilitarian uses of large capacity refrigerated centrifuge supplier have expanded due to technological advancements. It is utilized in pharmacology to ensure high-purity drug formulations. It is utilized in biotechnology for protein crystallization and vaccine synthesis. The extractive industry utilizes large capacity refrigerated centrifuge supplier to separate valuable minerals from raw mixture. In classrooms, it facilitates laboratory demonstrations of fluid flow. Even in the restoration of paintings, expert large capacity refrigerated centrifuge supplier facilitate cleaning and stabilizing delicate pigments. The applicability of large capacity refrigerated centrifuge supplier to so many different fields is evidence of its utility as an industrial and scientific agent for material separation.

{Keywords} of the future will unprecedentedly advance in performance and design. Future systems will feature adaptive balancing technology that adjusts to dynamic loads in real time. Intelligent rotors will track stress and fatigue in real time, allowing for extended service life. With IoT connectivity, multiple large capacity refrigerated centrifuge supplier units will be remotely managed to streamline laboratory networks. In biomedical applications, miniaturized devices will facilitate high-throughput screening with low sample volumes. These advancements are a step toward smarter, faster, and greener devices that revolutionize how separation processes are controlled in modern science.
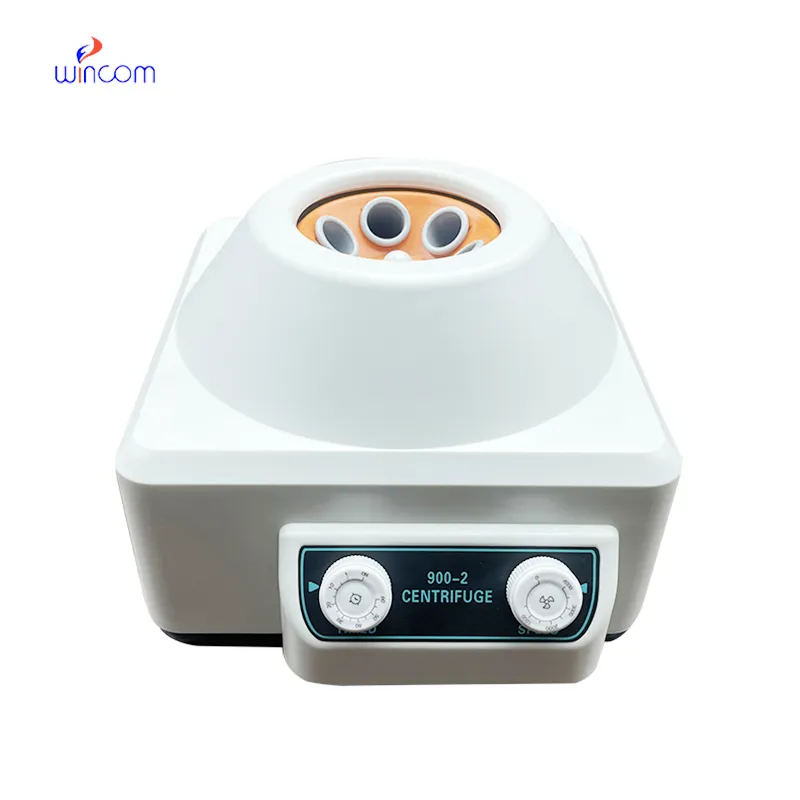
Routine maintenance of large capacity refrigerated centrifuge supplier begins with frequent cleaning and careful handling. Before each run, users should confirm that there are properly sealed, loaded tubes to prevent imbalance. The rotor, buckets, and seals should be washed gently and dried with air after each session. Periodic calibration checks ensure precise speed and temperature measurement. Rotor overloading is to be prevented since it will reduce motor life. With monitoring each maintenance cycle and adhering to safety protocols, laboratories can extend the functional life of large capacity refrigerated centrifuge supplier while ensuring precise performance.
A large capacity refrigerated centrifuge supplier is a universal gadget designed to separate parts in a mixture through sheer spinning power. A large capacity refrigerated centrifuge supplier operates through the principle of sedimentation, in which heavier particles move outwards and lighter particles remain at the center. Employed within laboratories, clinics, and industry in general, a large capacity refrigerated centrifuge supplier may be utilized to separate materials such as blood plasma, proteins, and chemical reagents with accuracy. Modern large capacity refrigerated centrifuge supplier exist in various forms, from benchtop to industrial types and ultracentrifuges, all for specialized applications. They are accurate and reproducible, a necessity in production and research.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
The delivery bed is well-designed and reliable. Our staff finds it simple to operate, and patients feel comfortable using it.
The centrifuge operates quietly and efficiently. It’s compact but surprisingly powerful, making it perfect for daily lab use.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We are planning to upgrade our imaging department and would like more information on your mri machin...
Hello, I’m interested in your water bath for laboratory applications. Can you confirm the temperat...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China

 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko